


2001 Starlinger Tape production line Starex 1000/105 + 1995 Sahm 230 GE winders for large coils + fibrillator
2001 Starlinger Tape production line Starex 1000/105 + 1995 Sahm 230 GE winders for large coils + fibrillator
Contact us for price
Location:Kraków, Poland
Description
Manufacturer: Starlinger
Model: Starex 1000/105 (STAREX 1000 unit for processing PP, HDPE, LDPE)
Type of machine: Tape production line
Year of manufacture: 2001
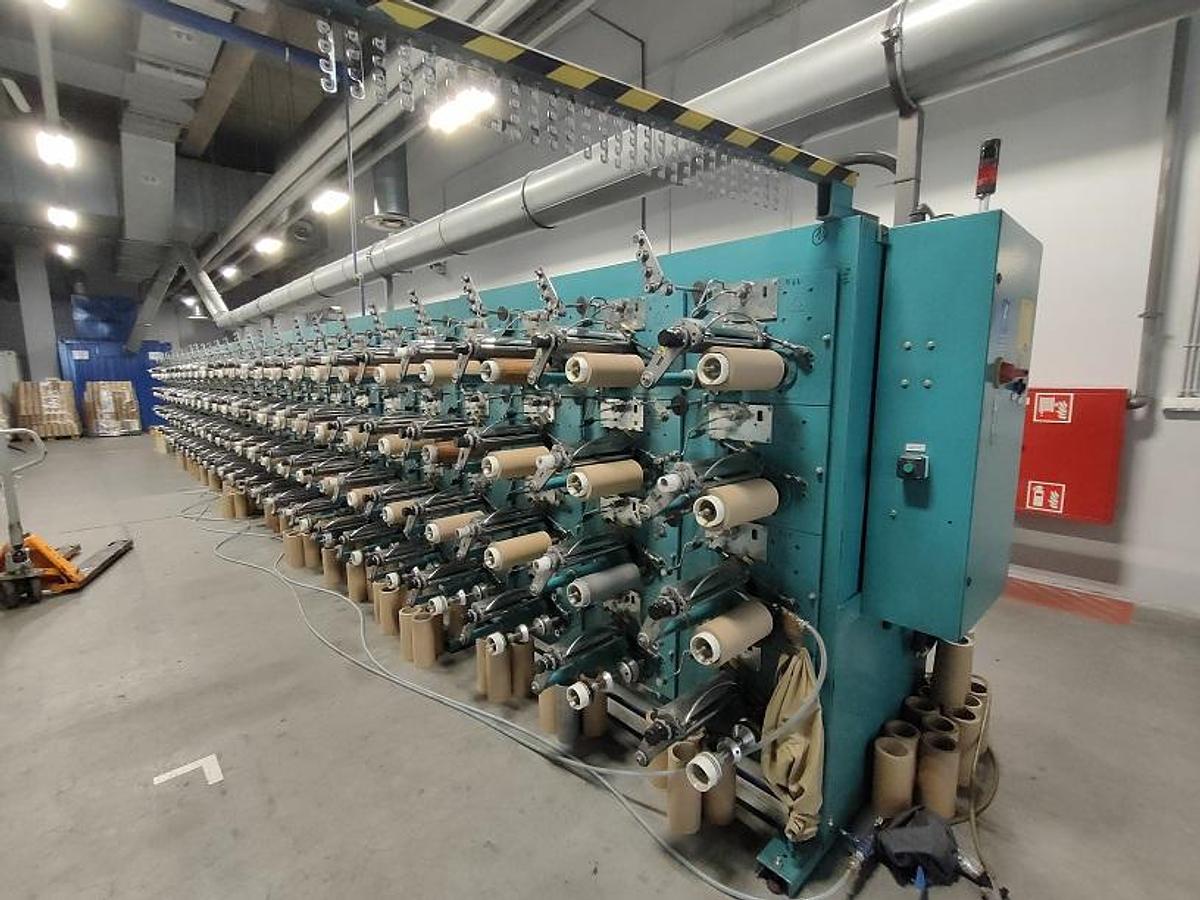
Includes: winders for large coils manufactured by Sahm 230 GE, 1995, and fibrillator
Technical Details:
- Slot width: 1100 mm
- Maximum working speed: 320 m/min
- Working width: 1000 mm
- Extruder type E 90.30 D: processing capacity of recommended material PP HC11 5FB by Borealis AG = max. 330 kg/h. Processing range for commonly used PP types with a melt flow index MFI approx. 2-5 g/10 min. Screw diameter D = 90 mm, screw length L = 30 D, screw speed n = 0 – 175 min-1, 6 heating zones, heating power approx. 37.8 kW, with 137 kW DC motor.
- Flat slot die: slot width 1100 mm, slot opening 0.1 - 1 mm, heating power approx. 14 kW, 6 controlled zones, with reversible lip.
- Tape cutting: razor blade slitting into tapes with widths from 1.7 – 4 mm, one complete spare cutter bar with 600 industrial razor blades.
- Water bath: capacity approx. 900 l with pump and heat exchanger, adjustable water level.
- Hot air chamber: air speed approx. 20 m/s, 4-meter long heating channel.
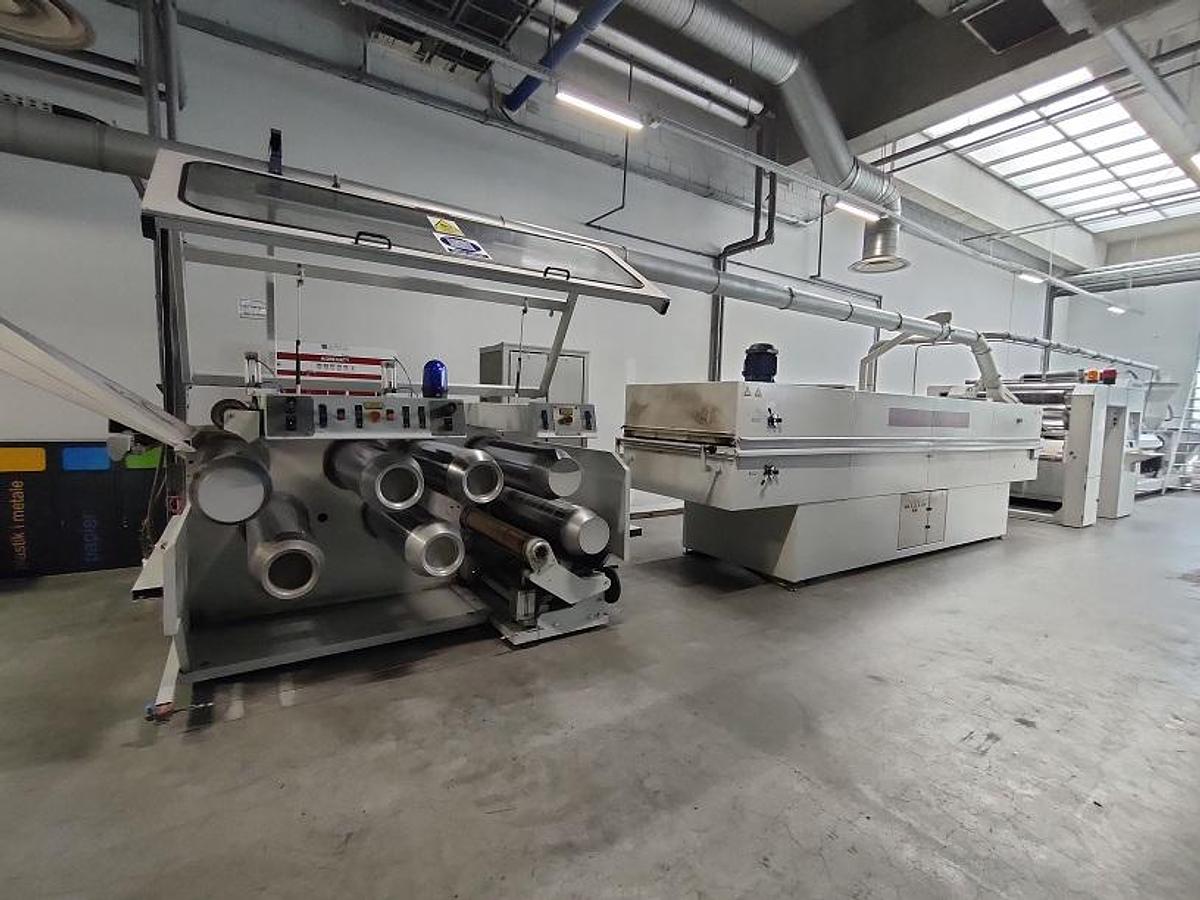
- Stretching unit with 5 godets: 3 standard godets with a diameter of 320 mm, 2 cooling godets with a diameter of 320 mm, 2 pressure rollers, deionizing unit, three-phase AC drive with frequency control, nominal power of 26 kW and additional three-phase AC drive with frequency control and nominal power of 6.9 kW, for individual setting of the draw ratio (version 1).
Main components and their function:
Extruder type E 90.30 D
• Processing capacity of recommended material PP HC11 5FB by Borealis AG = max. 330 kg/h
• Processing range for commonly used PP types with a melt flow index MFI approx. 2-5 g/10 min
• Screw diameter D = 90 mm
• Screw length L = 30 D
• Screw speed n = 0 – 175 min-1
• Number of heating zones: 6
• Heating power: approx. 37.8 kW
• With 137 kW DC motor
Extruder features
• Fully assembled on a common base frame
• Longitudinal extruder displacement on rail guides and rollers
• Main drive by DC motor via Cardan shaft
• Bimetallic cylinder with water-cooled feed zone
• Cooling blower and heating
• Nitrided hardened screw
• Special mixing and homogenizing zones
Production process control
• All control loops are centrally controlled
• Temperature regulation operates with self-optimization (automatic optimization system)
• Speed of individual drives along with the fibrillator is set via computer programming
• Recipe management, alarm system control, reporting machine parameters (speeds,
temperatures, draw ratios), machine parameter trend graphs
• Programmable controller and an industrial PC486 with a 14-inch monitor mounted on a swivel arm
• Temperature control start-up interlock for the main motor, to protect the extruder, filter, and flat die from cold start-up
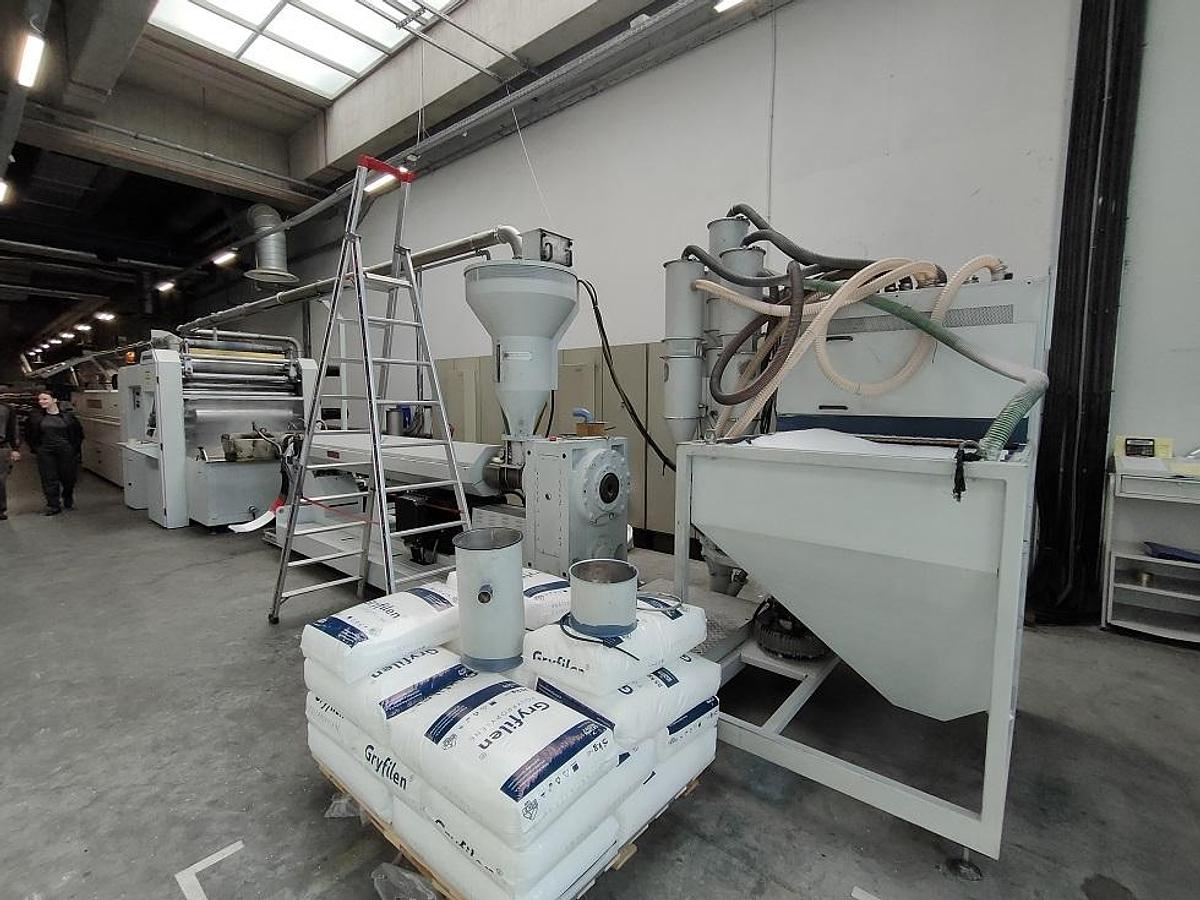
Pellet transport and dosing unit for three components
• Vacuum transport
• Elliptical dosing unit for continuous dosing and mixing of one main component and 2 additional ones
• Dosing of each additional component in the amount of 0.2 – 9% of the main component
Automatic filtration system
• Located between the extruder and the die, cleans the melted raw material mass
• Equipped with heaters
• Holds 20 m of filter belt
• Filter belt advance controlled depending on pressure (automatically) or manually by adjusting time and temperature
Melt pressure measurement device
• Located before the filter
• Combined device for measuring melt pressure and melt temperature before the die
Connections between extruder and die
• Static mixer
• Die connecting flange
• Die support stand / holder
Flat slot die
• Slot width 1100 mm
• Slot opening 0.1 - 1 mm
• Heating power approx. 14 kW
• 6 controlled zones
• With reversible lip
• Flexible lip, adjustable with clamping bolts
• Profiled flow channels in the form of a coat hanger
• With heating and complete cabling for PP processing
Edge trim removal
• Direct removal of narrow edge trims of un-stretched film to the extruder
• Consists of a cutting device and a system for conveying cut flakes back to the extruder hopper
Water bath combined with holding unit
• Capacity approx. 900 l with pump and heat exchanger, adjustable water level
• Film haul-off unit with pneumatically operated nip rollers, water removal system
• Pneumatically operated cutting unit with transverse adjustment
• Razor blade slitting into tapes with widths from 1.7 – 4 mm
• One complete spare cutter bar with 600 industrial razor blades
• Holding unit with 2 rollers and 2 pressure rollers
• Side frame with integrated operator terminal
Hot air chamber
• Adjustable heating zones
• Blowers, air speed approx. 20 m/s
• Airflow regulation
• Mechanically tiltable upper section
• 4-meter long heating channel
Stretching unit with 5 godets
• 3 standard godets with a diameter of 320 mm
• 2 cooling godets with a diameter of 320 mm
• 2 pressure rollers
• Deionizing unit
• Three-phase AC drive with frequency control, nominal power of 26 kW
• Additional three-phase AC drive with frequency control, nominal power of 6.9 kW, for individual setting of the draw ratio (version 1) Suction unit: aid during stringing-up and for monitoring tape breaks, system consisting of suction nozzles, transport pipes, and a waste container Control cabinet: air-conditioned, complete with internal cabling inside the unit
Fibrillator FC – 1000
• Used for fibrillating tapes, located between the 2nd and 3rd godet of a stretching unit
• Working width 1000 mm
• Max. tape thickness 70 microns
• Needle cylinder useful length 1000 mm
• 40 needle rows
• 13 needles per 1 cm
• Nominal motor power 10.6 kW
• Connected load 15.5 kVA
• Power consumption approx. 8.5 kW
Find more here - https://www.ucymachines.com/
Contact us at - sales@ucymachines.com
Specifications
| Condition | Used |
| Stock Number | 758772 |